
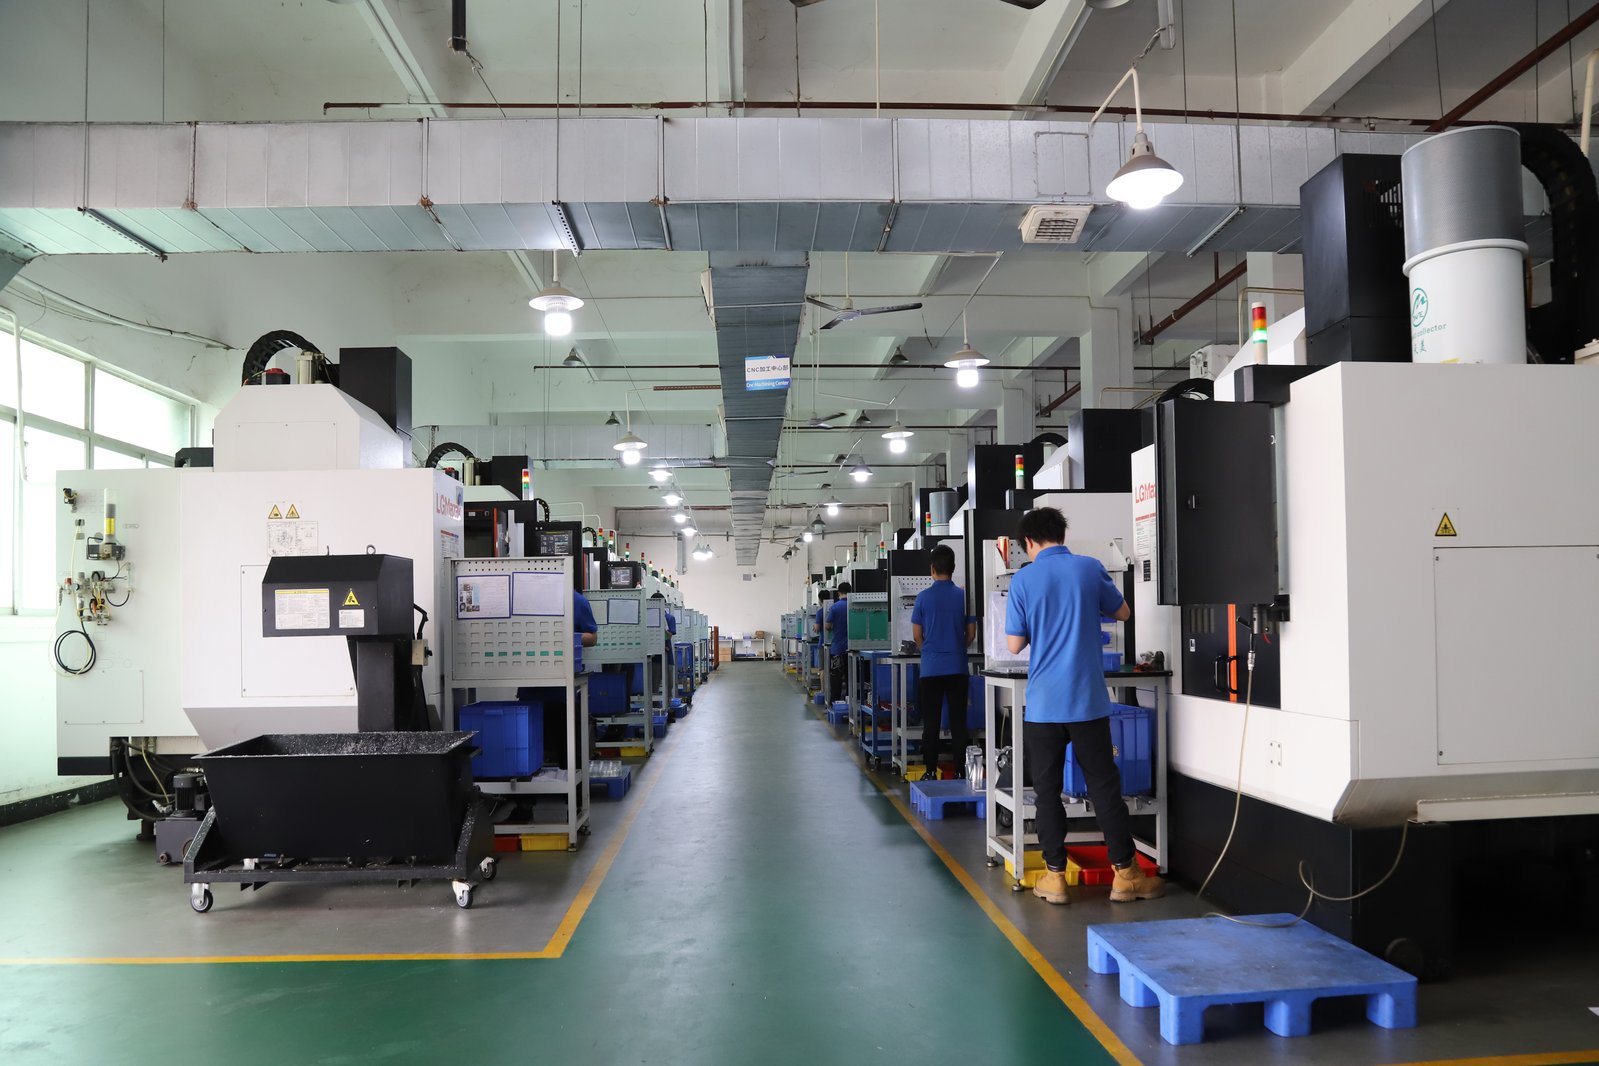
A large share of aerospace hardware is round before it is anything else. Fittings, valve spools, shafts, sleeves, couplings, and actuator bodies start as bar stock and take their identity on a lathe, with milling added for flats, slots, and cross-holes. For a buyer sourcing that work from a CNC turning and milling shop, the risk profile is different from plate machining: the geometry is axisymmetric, the critical relationships are concentricity and roundness rather than flatness across a face, and the material control story is written in bar stock and heat numbers. This guide walks the sourcing decision in the order it arrives — what makes the RFQ different, which alloys turn well under aerospace specs, what the process can hold, and what the lot must ship with.
What makes an aerospace turned or mill-turned part different from general precision work?
The turning drawing carries control requirements that a commercial part does not. The material is called out to an aerospace production standard with its condition, the certificate has to name the heat, and the drawing revision is a contractual fact because cutting from the wrong revision is scrap no tolerance can rescue. The flowdown from your customer — special requirements, first-article expectations, and the rule for deviations — has to reach the machine shop in writing, because a shop that never saw the flowdown cannot be held to it.
The engineering difference is axisymmetric discipline. A turned shaft's value lives in the relationship between features that share an axis: a bore concentric to an outer journal, a thread runout to the datum face, a groove square to the shaft centerline. When those features are cut in a single chucking or a single bar-fed cycle, the relationship is set by the machine's geometry; when the part is re-chucked for a second operation, the relationship is set by the operator's skill and the chuck's repeatability. That is why the first question to a turning shop is not what machines it owns but how it plans to hold the part, and how it verifies the runout numbers on the report.
Which aerospace alloys show up on turning drawings, and how do they behave on a lathe?
Turning drawings concentrate on a short list of bar-stock families, and each behaves differently when the tool is cutting around the axis. The table below is the practical starting point for a buyer comparing turning and milling services.
| Alloy | Typical turned parts | Turning notes | What to verify |
|---|---|---|---|
| 17-4PH stainless | Fittings, valve spools, high-strength hardware | Machines cleanly in the annealed state; age-hardened afterward, then finish-turned to control distortion | Age condition, heat-treat certificate, hardness |
| Ti-6Al-4V (Grade 5) | Lightweight fittings, shafts, thin-wall parts | Slow cutting speeds, heat stays at the edge, spring pass on thin walls; rigid bar support matters | Condition, heat number, straightness |
| Inconel 718 | High-temperature and turbine-area hardware | Severe work hardening; low speeds and hard tooling; chip control is a real problem on small bores | Heat-treat condition, mill source, lot traceability |
| 4340 / alloy steel | High-load shafts, landing-gear components | Machined soft, heat-treated, then finish-ground for final fits | Heat-treat certificate, hardness, plating record |
| 7075 / 2024 aluminum | Light housings, collars, non-structural fittings | Fast and stable to turn; 7075-T7351 bar holds thin sections without distortion | Temper, bar or forging form, certificate |
Three rules follow for a buyer. First, cycle-time honesty is the quickest capability test: a titanium fitting quoted at aluminum speed means the shop has not understood the material or plans to overrun the promise. Second, ask how the shop handles small deep bores in work-hardening alloys, because that is where turning jobs go wrong — broken drills and dimensional drift hide in the small-diameter features, not the big diameters. Third, remember that bar form matters: the straightness and hex or round tolerance of the incoming bar sets how much material the first operation has to clean up, and a bar certified to an aerospace spec costs more and protects the traceability story you will need later.
How do you stop alloy substitution and heat drift on turned bar stock?
Material control on a turning lot starts with the bar, not the drawing. The purchase order should name the alloy against its production standard — an AMS or ASME spec with the condition and form — and require the mill certificate to carry the heat or lot number. When the bar arrives, the shop logs it against the certificate and verifies the alloy with an incoming check such as XRF before the first part is cut. The heat number then follows the work order, so every part in the lot is traceable to a specific bar and a specific certificate.
The less visible risk is heat-treat drift. Many aerospace turning alloys are machined in a soft condition and aged afterward — 17-4PH and Inconel 718 both move during aging, which is why the finish turning happens after the heat treatment and why the drawing and the work order have to agree on the sequence. When the heat treatment is subcontracted, the processor's certificate becomes part of your lot record, and the shop should name the processor in the quote rather than discovering it at the audit. A supplier that can show the chain — bar certificate, incoming verification, heat-treat record, final inspection — is giving you the traceability an aerospace auditor recognizes; one that cannot is asking you to trust the last link by faith.
What tolerance and roundness can turning hold, and when is grinding the honest answer?
The honest numbers do not change because the part flies. Production turning and milling hold fit and alignment features to ±0.003 mm, precision grinding reaches ±0.002 mm, and suppliers demonstrate capability of Cpk 1.67 or higher on key characteristics and Cpk ≥ 1.33 on general characteristics. Capability is reported per characteristic: every report names the feature, its tolerance band, the sample size, the sigma method, and the study window. On a turned part, the key characteristics are usually the journal diameters, the bearing seats, and the bore-to-OD concentricity — the features that mate, rotate, or seal. Those are the features that deserve the tight band; the general envelope runs at a block tolerance.
Roundness is where turning meets its limit. A lathe produces a part that is round within the machine's accuracy and the chuck's condition, and for most fits that is enough. But a journal that must be round in the low microns, with a mirror-class finish, is a grinding job — the honest quote separates the turning from the grinding operation and prices both. The same logic applies to features that must be square to the axis to a few microns, where a second grinding or finishing pass on the face is the process that delivers it. When a drawing asks for better-than-turning numbers on a turned feature, the right supplier response is a process proposal, not a silent acceptance, and that response is a good early signal about the rest of the order.
Which surface finishes and thread requirements matter on aerospace turned parts?
Finish on a turned part follows function, and the drawing should say so by feature group. A machined finish around Ra 3.2 µm is fine on non-contact surfaces; journals and seal faces carry Ra 1.6 µm or better, and below Ra 0.8 µm the honest processes are grinding or polishing, not turning. Add the direction question: turning leaves a characteristic spiral lay, so if a seal requires a non-directional or cross-hatched surface, the process that produces that lay has to be named rather than assumed.
Threads deserve their own callout because they are the most inspected feature on a fitting and the easiest to under-specify. Name the thread standard on the drawing, and state how it will be verified — calibrated plug and ring gages for the fit, with thread form checked against the standard. Ask whether critical threads are single-pointed, rolled, or chased, because the process changes the fatigue behavior of the part and the record should say which one was used. When a fitting is the pressure boundary of a hydraulic line, the thread is not a detail; it is the seal, and its inspection record belongs in the lot documentation next to the material certificate.
What documentation should an aerospace turned-and-milled lot ship with?
The shipping package for an aerospace turning lot should read like a chain, with every document naming the same purchase order, heat, and work order. The core set: the material certificate with the spec, condition, and heat number; the incoming verification record tying the certificate to the physical bar; the heat-treat certificate when aging or solution treatment is part of the route; the first-article inspection report covering every characteristic on the drawing; the dimensional report with runout, roundness, and true-position values for the key characteristics; and the certificate of conformity binding the lot to the purchase order.
Check the dimensional report for the numbers you actually asked for. A turning report should show the journal diameters, the bore and OD runout values, the thread gage results, and the surface finish readings on the called-out features, not a single "all dimensions conform" line. If a feature is critical enough for a tight band, it is critical enough for a measured value, and an aerospace inspector will want to read that value on paper rather than trust it to memory. Agree this list in the RFQ so the report is produced to your template, not improvised at the dock.
What should you verify on a turning shop before awarding aerospace work?
Start with the quality system and verify it by number with the registrar — a system such as ISO 9001:2015 is the common baseline for component machining, with IATF 16949:2016 (product design excluded) for automotive and ISO 14001:2015 for environmental management, and aerospace programs often flow down AS9100 or equivalent from the customer. Then look for the inspection equipment that turning quality actually depends on: a coordinate measuring machine for the position and true-position features, surface roughness measurement for the Ra callouts, and roundness or cylindricity capability for the journals that need it. A turning shop that measures roundness on a V-block and calls it good is not equipped for the tight-journal part on your drawing.
Ask for the machine-side evidence of control: calibration records for the CMM, gages, and thread rings; a material storage area that keeps certified bar segregated by heat; and a non-conformance process that quarantines and documents rather than quietly reworks. Then ask for a redacted sample of a completed lot's paperwork and read it as an auditor would: does the certificate name the heat the CMM report claims, and does the report list measured values for the features your drawing would call critical? A live video walk-through of the turning cells and the inspection room completes the picture, and the quality page on this site explains how inspection, calibration, and documentation are handled as part of the service.
How do you write the aerospace RFQ for turned parts so quotes are comparable?
Write the RFQ as a specification, not a description. Attach the drawing at a named revision with the GD&T datum structure, and call out the concentricity or runout relationships explicitly — on a turned part the axis is the datum, and the callouts should say so. Name every material by spec, condition, and form, and require the mill certificate with the heat number. State the surface finish by feature group, name the thread standard and its inspection method, and list the documentation you expect with the lot. Ask the supplier to confirm, line by line, which tolerances it holds, which features it would route to grinding, and which process steps are subcontracted.
Then read the confirmation for specificity. A supplier that answers "we hold ±0.003 mm on the turned diameters, we recommend grinding on the two journals, we verify threads with calibrated ring gages, and our aging is done by an approved processor" is engineering your part; one that confirms everything with no questions has quoted the drawing without reading it. The parts guide shows how tolerance and finish callouts land on a quoted turned part, and the FAQs cover quoting and batch economics. When the confirmation and the audit agree, the remaining risk is manageable, which is the entire point of doing the paperwork before the purchase order.
Frequently Asked Questions
How do I know a turned part's concentricity is held rather than best effort?
Ask how the features are cut and measured. A part that holds its bores, journals, and threads in one chucking, with runout values reported on the inspection sheet, has a measurement trail you can audit. Demand the actual runout numbers for the features your drawing calls out — a report without them is not evidence.
Can mill-turn machining finish an aerospace part completely in one setup?
For most turned-and-milled parts, yes — diameters, faces, grooves, threads, and off-axis features cut with the part held once. The exceptions are features that need a different process class, such as a journal that demands grinding. The quote should name those exceptions instead of forcing the part through one machine.
Which alloy should a high-pressure aerospace hydraulic fitting be made from?
17-4PH in a condition such as H1025 is the usual answer: it machines from bar, ages to consistent strength, and resists corrosion. Ti-6Al-4V is chosen when weight or temperature rules the design. Name the grade with its condition and heat-treat state on the drawing so the certificate can be checked against it.
How tight a tolerance should I put on a turned aerospace shaft?
Put the tight band on the features that mate or rotate and run the rest at a block tolerance. Turning holds fit and alignment features to ±0.003 mm, and precision grinding reaches ±0.002 mm where a journal needs roundness and finish beyond turning, with Cpk of 1.67 or higher on key characteristics and Cpk ≥ 1.33 on general characteristics. Capability is reported per characteristic: every report names the feature, its tolerance band, the sample size, the sigma method, and the study window. Tightening everything raises cost without improving the shaft.
What should I specify for thread quality on an aerospace turned part?
Name the thread standard and its verification method. Structural threads are verified with calibrated plug and ring gages, not a visual pass. Ask whether critical threads are single-pointed, rolled, or chased, because the process affects fatigue behavior, and record the choice in the inspection report.
How is raw bar stock verified and traced on an aerospace turning lot?
Incoming bar is logged against its mill certificate, checked by alloy analysis such as XRF, and the heat number follows the work order so each part traces to its lot. Aerospace programs often require bar certified to an AMS or ASME spec. Ask for the incoming verification record before you trust the certificate.
When is a forged blank better than machined-from-bar for an aerospace turned part?
When the part is large enough that machining from bar wastes costly material, or when the application needs the grain flow of a forging. Small fittings and shafts are usually more economical from certified bar. The crossover depends on diameter, length, and alloy price — ask for both routes on the quote.
Qualifying a turning and milling shop for aerospace work?
Email [email protected] or call +86 13126536955 and ask the audit questions directly — material verification, concentricity, thread control, and what a lot ships with.