
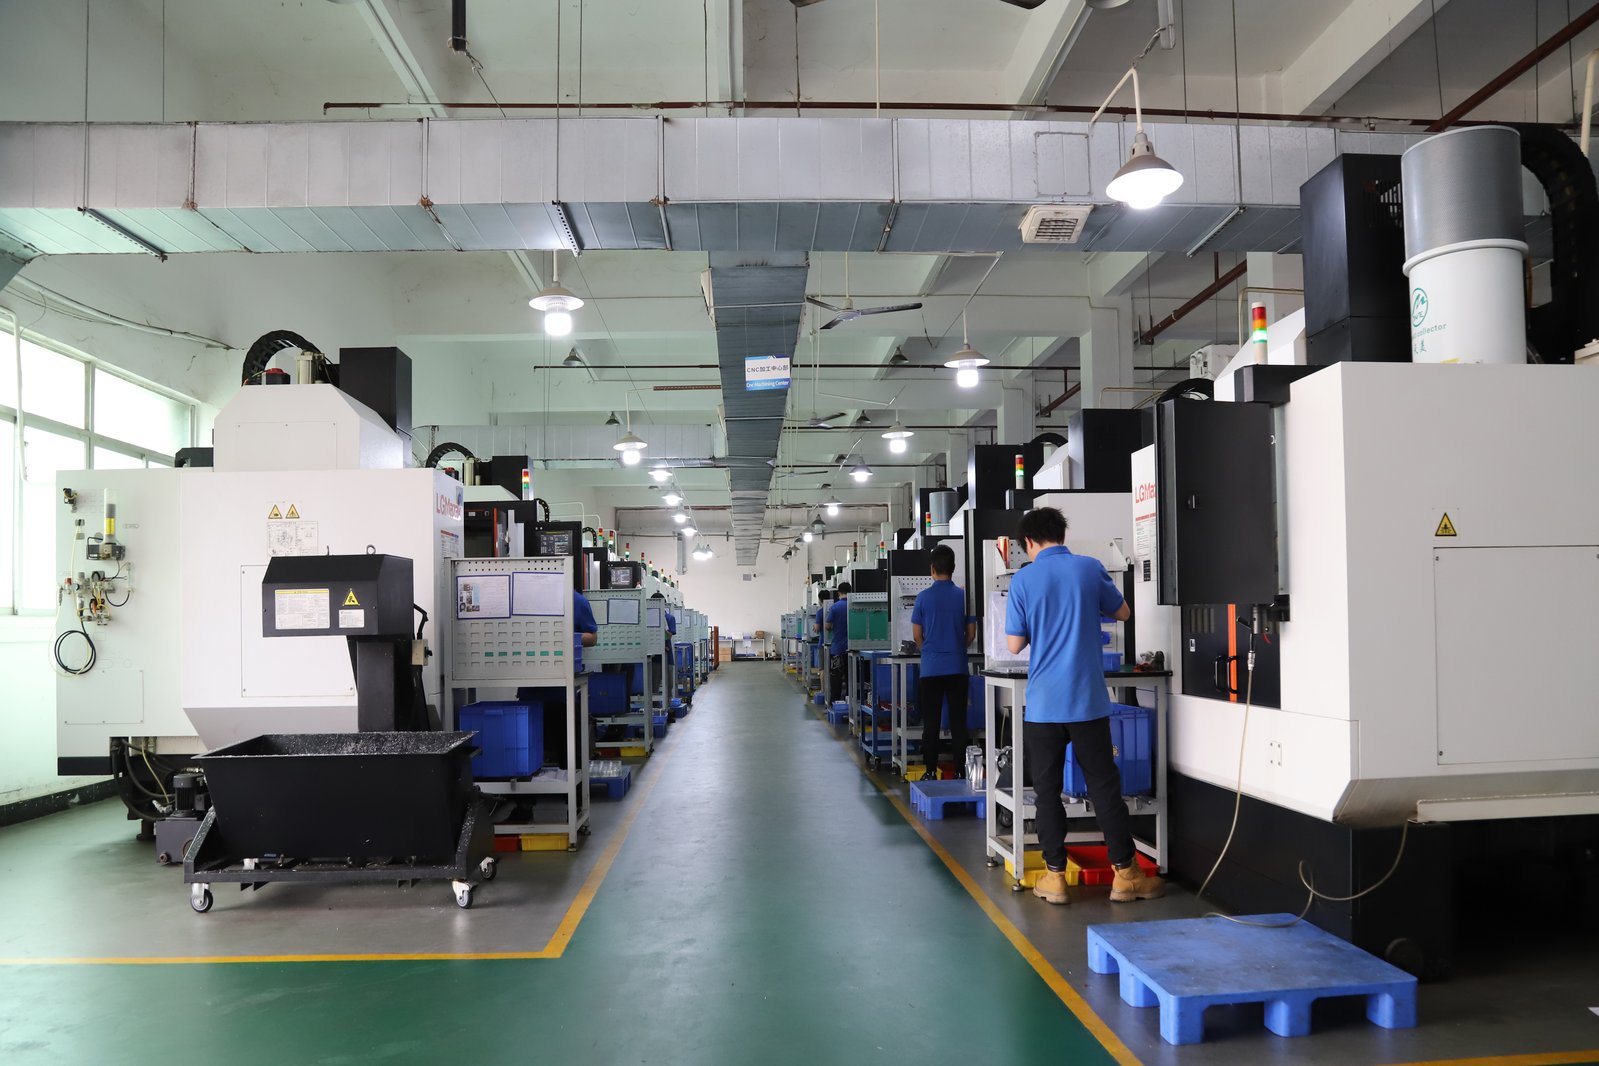
The common advice about tolerances treats a part as one object, but a part that is both turned and milled is really two jobs sharing one drawing. Turning produces diameters, roundness, and circular surfaces that live on the axis of the bar; milling produces flats, pockets, and hole patterns that live on planes and datums. Each process holds its own bands - on the order of ±0.003 mm for the controlled features of both, with ±0.002 mm achievable where grinding follows - and each leaves its own surface texture. A buyer who knows which callouts belong to which process can write a drawing the shop executes without guessing, and a supplier that machines both can tell you which feature will cost more before it is cut.
- Two processes, one drawing: turning owns the axis work, milling owns the planes and patterns, and each holds about ±0.003 mm as standard.
- Ground details go finer: about ±0.002 mm where a surface seats or seals and grinding follows.
- Capability is the proof: Ppk ≥ 1.67 initial on the characteristics your drawing marks critical.
- Finish follows the operation: turned faces carry a circular lay, milled faces carry the toolpath texture.
- Plan the datums once: a feature measured between two operations needs a datum story that survives the setup change.
Why does it matter which process makes a feature?
A turned diameter and a milled slot are both machined, but they are produced by different kinematics and measured against different references. A diameter is cut by the rotation of the bar and is naturally round relative to the axis; a slot is cut by a moving tool and is defined by its position on a plane. Holding the diameter tight is a turning problem, and holding the slot position tight is a milling problem.
When a drawing does not distinguish them, the shop still does, because the operations run on different machines or in different steps. The practical consequence is that the quote and the inspection plan separate along the same line: axis features verified in the turning step, planar features verified after the milling step.
The same split belongs in the drawing notes. A note that lists which features are turned and which are milled removes guesswork from quoting, because the shop no longer has to infer the intended process from the geometry alone.
Knowing the line is useful to a buyer because it predicts where the cost sits. A tight diameter on a long bar costs turning effort and workholding care; a tight hole pattern on a milled face costs positioning and datum discipline. Asking for both at once on one feature is where budgets quietly double.
What bands should you expect from the turning side of a shop?
Turning work holds the familiar production values: diameters and turned lengths around ±0.003 mm, with roundness and concentricity controlled by the workholding and the cut. Grinding, where the drawing calls for it, takes seat and seal surfaces to about ±0.002 mm.
The turning side also owns the surface texture of axis work. A turned face carries a circular lay - the tool marks run around the part - which is the natural texture for a journal or a seal surface that rotates. Naming a finish on a turned diameter is really naming the finishing pass the lathe must make.
Slender work is where the turning side earns its reputation. A long shaft flexes under the tool, so tight roundness along the length needs support - a steady rest, a sub-spindle, or a carefully sequenced cut - and the quote should reflect the support the geometry demands.
Threads belong to the turning conversation as well. A thread that must engage a mating part is produced in the turning step with its own tooling and verification, so its pitch and position callouts travel with the axis work rather than with the milled detail.
What bands should you expect from the milling side?
Milling holds the same order of band on its own features: flats, pockets, slots, and hole patterns around ±0.003 mm, with the fine end of that range reserved for the features a drawing marks critical. The challenge on the milling side is not the value but the reference, because a milled feature is positioned against datums rather than against the bar axis.
Position tolerances on hole patterns and slot locations are verified on a CMM against the datum structure, and the datum structure is where good drawings are made or broken. Datums that are machined, reachable, and unambiguous produce reports that can be checked; datums that live on curved or cosmetic features produce arguments.
When datums must move, say so. A part whose drawing datum is a turned face but whose final datum is a milled surface needs the relationship between the two stated, or the inspection report will measure against the wrong reference.
Milled surfaces carry their own texture, set by the toolpath and the stepover. A finish note on a milled face is a request about the last pass, and the shop plans the toolpath to leave the texture the drawing names.
A milled face finish is only as stable as the tool that cuts it, so a drawing that cares about texture should ask about tool-change frequency rather than assume the first article will repeat forever.
Where do roundness, concentricity, and datum structure come in?
Roundness and concentricity are the callouts that connect a turned diameter to the part it belongs to. Roundness describes how close a section is to a true circle, and concentricity or runout relates one diameter to another or to the datum axis, which makes them the features that decide whether a shaft spins true in an assembly.
Measuring them is a CMM or roundness-tester job, and the measurement needs the datum story the drawing provides. When a part is turned, then milled, the datum axis established in the turning step must survive the setup change into the milling step, or every position reading on the milled features drifts with it.
The drawing should state the datum order plainly, because a CMM measures in the order the datums are listed. Two shops reading the same drawing can produce different numbers if the datum order is not explicit, and the difference lands in the acceptance argument.
Ask the shop to show the datum strategy in the design review. A supplier that can describe how the axis survives the setup change is one that has run mixed parts before; a shop that cannot is about to learn on your order.
How do surface finishes differ between turned and milled faces?
A turned face and a milled face both come off the machine in the Ra 0.8 to 3.2 range, but the texture is shaped differently. Turning leaves a circular lay that suits rotating seals and journals; milling leaves the toolpath pattern, which suits faces that clamp or sit flat against another part.
The function should choose the process note. A face that must seal against a rotating shaft is naturally a turned face with its circular lay; a face that must seat a gasket is naturally a milled face whose flatness is controlled. Writing the finish without the operation can invite the wrong texture.
Where a finer value is needed, grinding follows whichever operation produced the face, and the drawing should say when the roughness is measured - as machined or after any coating - because plating and anodizing change the surface after the tool leaves it.
Where both textures appear on one part, keep them on separate notes. A face that is turned for the seal and then milled for a detail should carry two finish notes or a clear statement of which surface governs, so the operator does not guess.
Which tolerance and finish combinations belong on the same callout?
A functional surface usually needs both a size or form tolerance and a finish, because the two are produced by the same pass and tested by the assembly together. A bearing journal needs its diameter, its roundness, and its surface in one package; a gasket face needs its flatness and its roughness as a pair.
Separating them across the drawing is a common and expensive error. When the size callout is on one view and the finish on another, the shop may hold one and miss the other, and the first article returns the lesson with an extra machining cycle attached.
The remedy is to group them: on the feature itself, state the size or form value, the roughness, and the process condition in one note. A reviewer can then see at a glance what the feature must be, and the inspection plan inherits the same grouping.
Resist copying the group from one feature to its neighbours. Similar features often have different functions, and a group copied by habit spreads fine callouts across the drawing without adding value to the assembly.
What evidence should a mixed turning-and-milling part carry?
A part machined in both operations should carry evidence from both. The first-article report should show the turned diameters with their roundness and concentricity readings, and the milled features with their position and finish values against the drawing datums, each measured with the instrument that fits the callout.
The report should also carry the drawing revision and the material heat number, so the part that was measured is the configuration that was approved. On a mixed part, the revision matters doubly, because a change to a milled feature can affect the turning setup and vice versa.
Keep a change log next to the report. When a revision moves a milled feature, the log shows what was measured before and after, which turns a disagreement about numbers into a discussion about what changed.
Record who approved the change and when. A report without an approval trail is a set of numbers; with the trail, it is a decision history that answers most audit questions before they are asked.
After the first article, the evidence steps down to the criticals and a conformance line for the rest, but the stepping-down rule should be agreed in the order. A supplier that knows the evidence requirement before it quotes builds the inspection into the process rather than bolting it on at the end.
How do you set the bands so both operations stay affordable?
The budget rule is the same as anywhere: hold the fine band where the assembly depends on it, and let the rest live on a stated general block. On a mixed part, apply that rule per operation, because a fine callout that costs little in one step can cost a lot in the other.
Finally, remember that the general block applies to both operations equally. State one block that covers linear, angular, and radial features, so the turned side and the milled side are quoting to the same default.
Once the two sides of the drawing are clear, ask the shop to quote them separately. A quotation that shows turning cost and milling cost as their own lines, rather than one blended total, makes the process budget visible and the next revision cheaper to price.
- Separate the criticals by process. Mark which fine features are turned and which are milled, so the quote and the inspection follow the operation that owns each one.
- Plan the datum story first. A datum structure that survives the change from turning to milling avoids re-fixturing arguments and CMM disputes.
- Group size and finish per feature. Put the form or size value, the roughness, and the process condition in one note on the feature.
- State the finish timing. Say whether the roughness applies as machined or after coating, and which operation produces the face.
- Ask for capability per critical. Ppk ≥ 1.67 initial on the features your drawing marks key, demonstrated from the first lot.
A drawing that respects the two processes reads as two jobs sharing one page, and a shop that machines both will tell you which side of the drawing carries the cost. That is the conversation a realistic specification is meant to start, and the first article is where it finishes.
Frequently Asked Questions
Can a turned-and-milled part hold ±0.003 mm across both operations?
Yes. Turned diameters and milled features each hold around ±0.003 mm in a controlled process, and ground details reach about ±0.002 mm. The capability expectation of Ppk ≥ 1.67 initial applies to the characteristics your drawing marks critical.
Why does a milled slot cost more to position than a turned diameter costs to size?
A turned diameter is defined by the bar rotation and is naturally round; a milled slot is positioned against datums on a plane and needs a CMM setup to verify. The reference system, not the machine, drives the difference.
What finish does a turned surface leave compared with a milled one?
Both start in the Ra 0.8 to 3.2 range. Turning leaves a circular lay suited to rotating seals; milling leaves the toolpath texture suited to faces that clamp or seat flat against another part.
Should I specify roundness on a turned diameter?
Yes, where the function needs it - a journal that spins in a bearing, for example. Roundness and concentricity are verified with a CMM or roundness tester against the datum axis, and they add their own inspection cost.
What does as-machined versus after-coating mean for a finish?
As-machined is the texture the tool leaves; after-coating is the texture once plating or anodizing has changed the surface. The two rarely agree, so the drawing should state which condition the roughness applies to.
What should the first article show on a mixed part?
The turned diameters with their roundness and concentricity, the milled features with their position and finish against the datums, the drawing revision, and the material heat number - the evidence from both operations in one report.
Why does datum order matter in the inspection report?
A CMM measures in the order the datums are listed, and a different order can produce different numbers. The drawing should state the datum order so two shops reading it agree on what the report means.
Need the bands set for a part that is both turned and milled?
Send the drawing with your critical list and ask for a review that separates the turned and milled callouts and prices each side before you commit. Contact the CNC Turning and Milling team to start.